Drum Motor Selection Parameters: A Technical Guide to Torque, Belt Speed, and Roller Width
Drum Motor Selection Parameters: A Technical Guide to Torque, Belt Speed, and Roller Width
A drum motor is a conveyor drive in which the electric motor, the gear stage and the bearings are built into the drum shell, so the shell itself acts as the drive pulley. Because the drive is fully enclosed, selection comes down to three parameters that have to be fixed together: the torque delivered at the shell, the nominal belt speed, and the roller (face) width. A conveyor that slips, stalls, mistracks or runs at the wrong throughput is usually the result of one of those three being matched to the wrong condition, not of the drive being unsuitable in principle.
This guide is written for conveyor designers, maintenance engineers and procurement teams specifying light-duty packaging lines and hygienic food, pharmaceutical or washdown conveyors. It explains how each parameter is defined, how the three interact, which project data to collect before contacting a supplier, and how to read the values on a supplier data sheet. Market and compliance figures are attributed to their sources; where a value depends on the individual conveyor, the calculation method is given instead of a generic number.
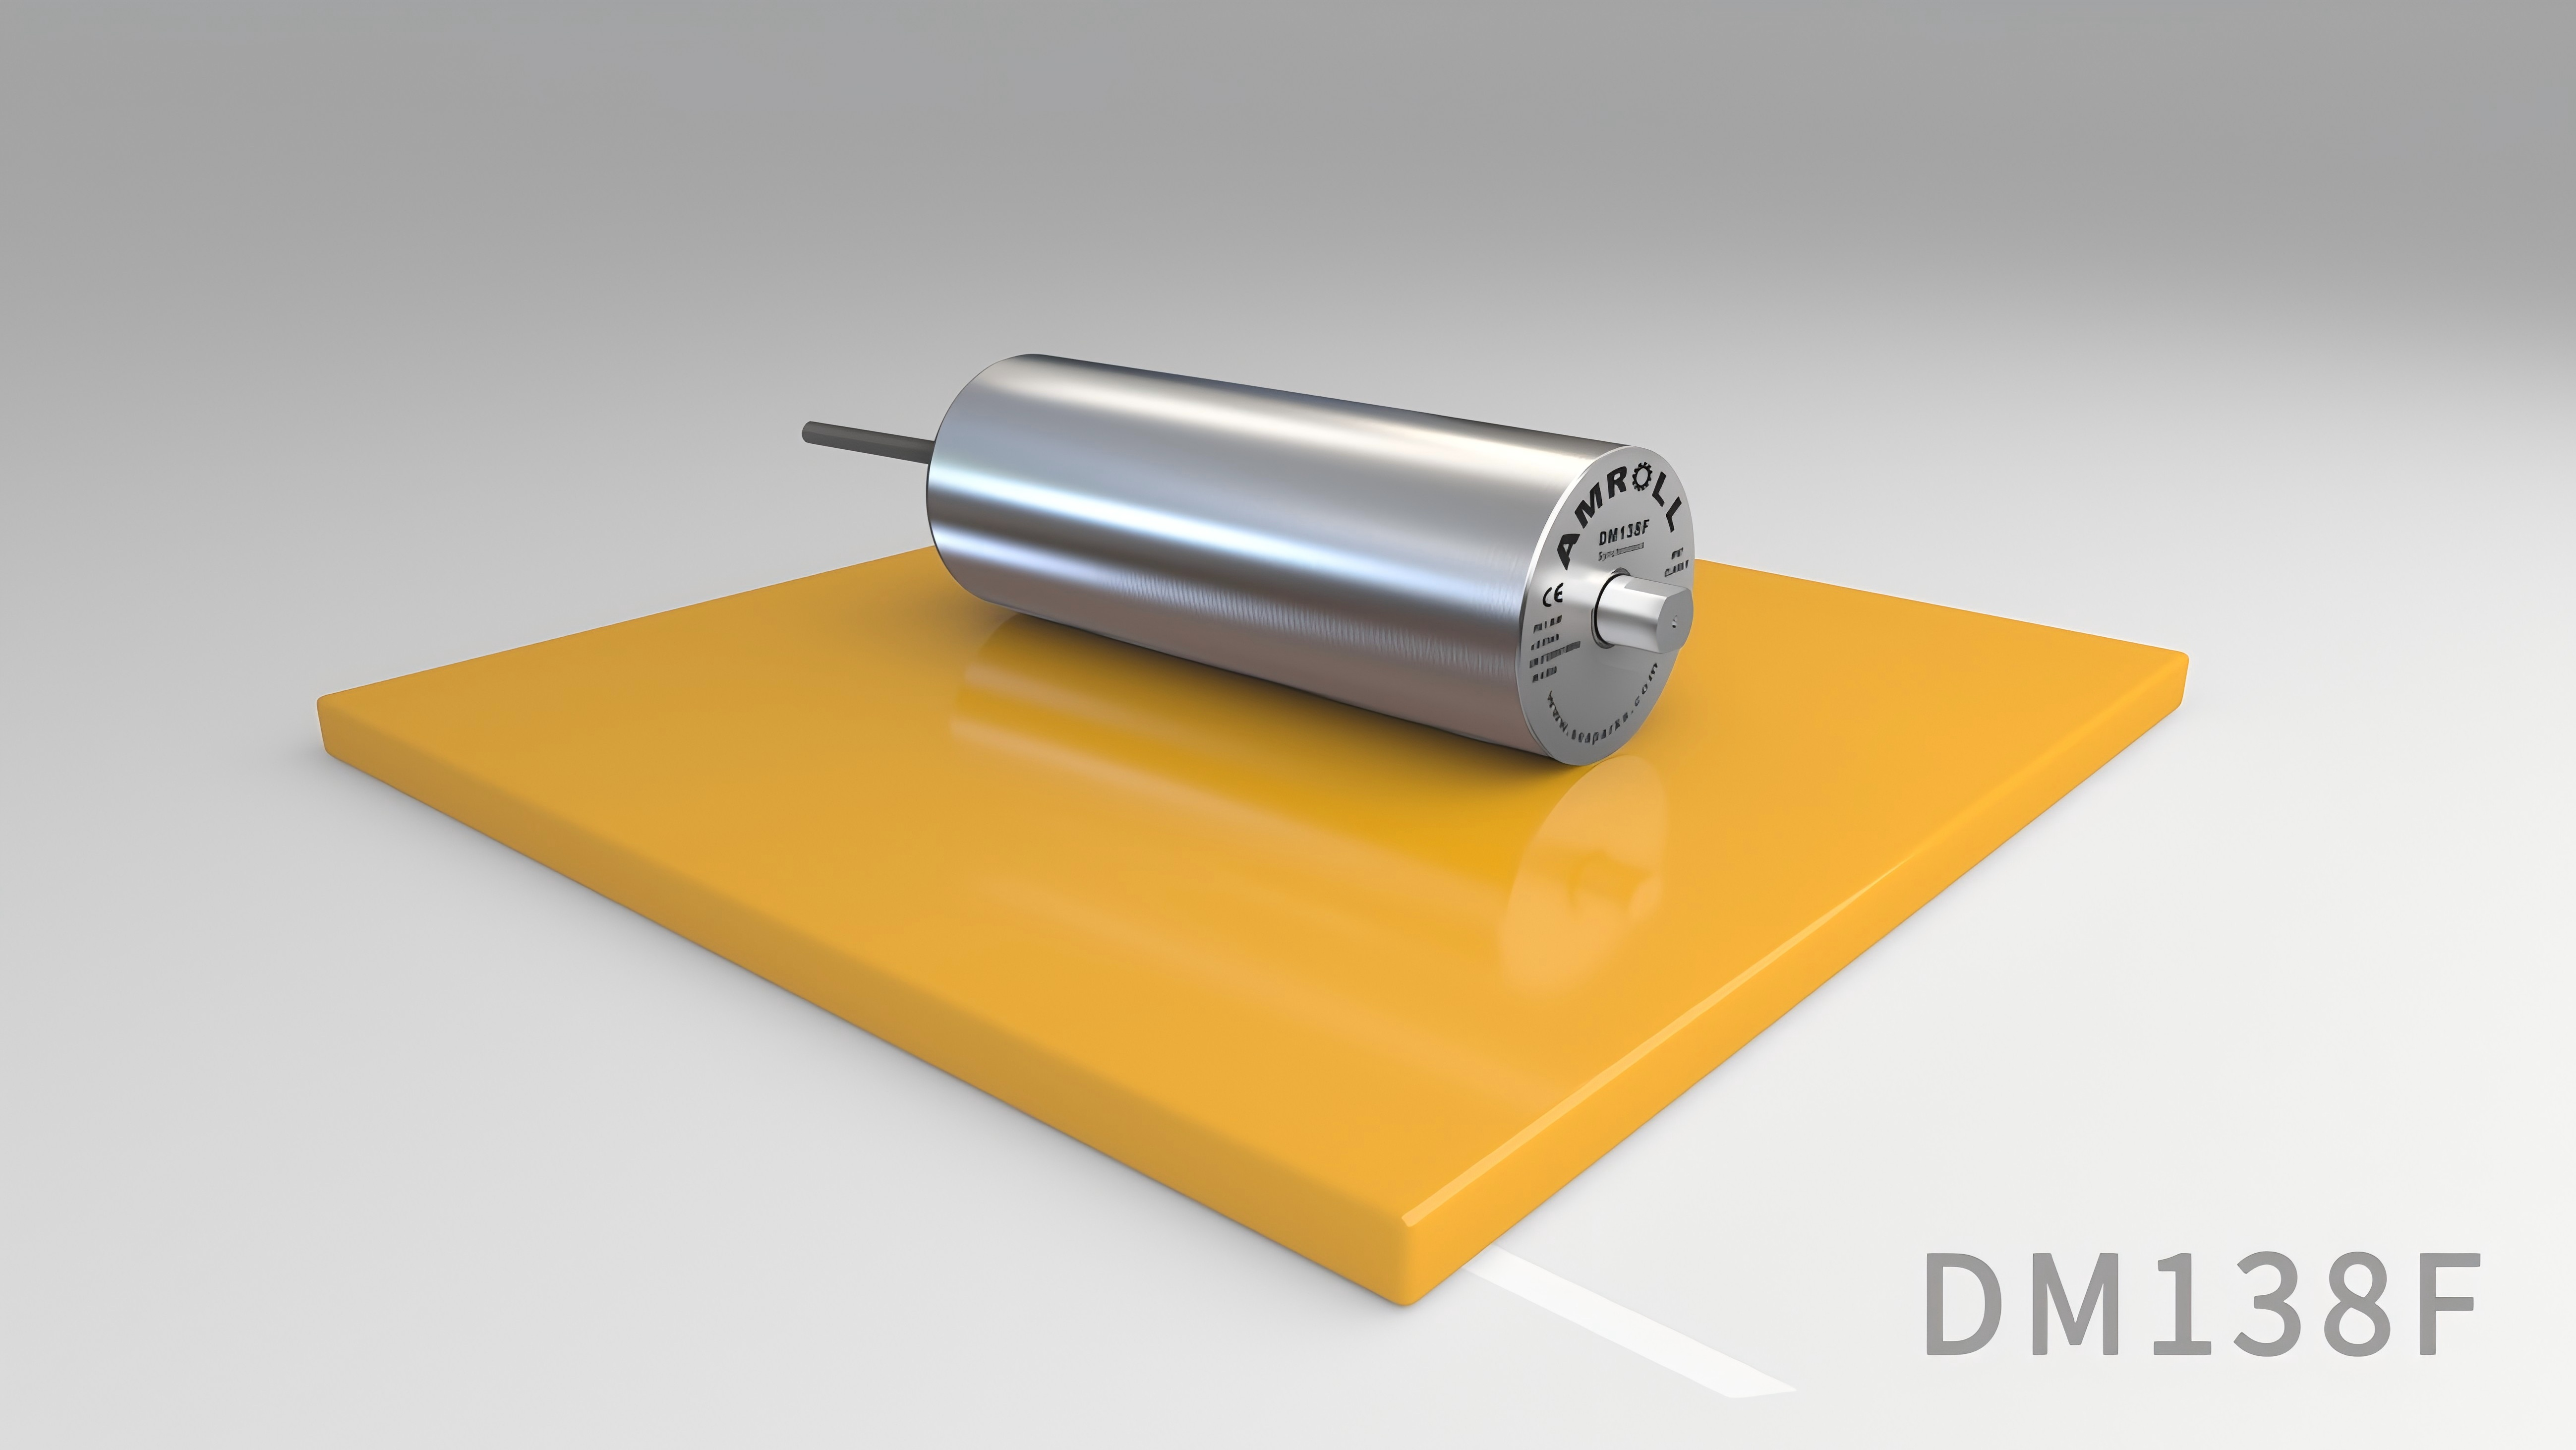
A drum motor product diagram: motor, gear stage and bearings sit inside the shell, so torque, belt speed and roller width are all fixed on the drum itself.
Problem Definition: Why Drum Motor Selection Goes Wrong
Most specification errors repeat themselves across projects, and they usually appear in one of five forms.
- Torque copied from another line. Two conveyors with the same belt width can carry very different loads, inclines and start-up frequencies, so a torque figure that works on one line can slip on the next.
- Belt speed chosen from throughput alone. Nominal belt speed also governs product stability at transfers, accumulation behaviour, and compatibility with inspection or screening equipment.
- Roller width treated as a formality. The face width has to support the belt across its full width inside the frame, with the correct edge clearance. Too narrow and the belt edges are unsupported; too wide and mass, cost and tracking behaviour change.
- The three parameters treated as independent. For a given motor power and drum diameter, a lower nominal belt speed produces more torque at the shell, and a higher belt speed produces less. Torque and speed have to be fixed as a pair, and the roller width defines the surface over which that torque is transmitted.
- Environment considered after the drive is chosen. A drive that cannot cope with the plant cleaning regime forces a redesign, or creates a permanent cleaning burden that was never priced into the project.
The symptoms of a mis-selected unit are consistent: belt slip on the shell, overload trips at start-up, product toppling at transfer points, damaged belt edges, and - in hygienic areas - product accumulation around a drive that cannot be cleaned effectively. None of these are solved by buying a larger motor; they are solved by re-deriving the three parameters from the conveyor itself.
Industry Background: Why These Parameters Are Compared More Carefully Now
The drum motor has moved from a niche alternative to a mainstream conveyor drive. The global drum motor market was valued at approximately USD 2.07 to 2.13 billion across 2023-2025, with growth attributed to logistics automation and food processing demand (Custom Market Insights). Published estimates diverge - Dataintelo places the 2025 figure at USD 2.8 billion and Market.us at USD 2.0 billion - largely because reports include different amounts of ancillary conveyor components. For a buyer, the practical reading is that the category is large, competitive and increasingly well documented, which makes parameter-level comparison realistic rather than anecdotal.
Two structural facts shape what is being compared. First, AC motors dominate the category: the AC motor segment held a 52.3% revenue share in 2025 (Dataintelo). Second, the demand centre is shifting east, with Asia Pacific the fastest-growing region and a projected 38.2% revenue share by 2025, driven by industrialisation and e-commerce growth in China and India (Dataintelo). On the supply side, Interroll is identified as a leading player in the drum motor market, while Van der Graaf, reported at approximately 7.8% of the global market, concentrates on heavy-duty drum motors for mining and aggregate duty (Dataintelo).
Efficiency has become a selection parameter in its own right. Energy-efficient drum motors can achieve overall efficiency of up to 82-83%, which changes total cost of ownership calculations against traditional geared motors (Rulmeca / Interroll). Compliance has tightened in parallel: drum motors placed on the European market must comply with the Low Voltage Directive 2014/35/EU and carry the CE mark, often referencing safety standard EN 62841 or IEC 60034-1 (European Commission). For hygienic applications, IP69K under IEC 60529 is the highest ingress protection rating and is the rating used where equipment must withstand high-pressure washdown up to 1450 psi and temperatures around 80 degrees Celsius (IEC / IBT Industrial Solutions).
Shell diameter, face width and shaft arrangement are the physical dimensions behind the three selection parameters.
Detailed Solution: Matching Torque, Nominal Belt Speed and Roller Width
Selection starts from the conveyor, not from a catalogue page. The three parameters are derived from the load, the process and the frame, and only then compared with what a supplier can offer.
1. Torque: what the shell has to turn
Torque is the turning moment the drum must deliver at its shell to move the loaded belt. It has to cover four things at the same time: friction between the belt and its support (slider bed or carrying rollers), the mass being conveyed, internal losses in the drum bearings and gear stage, and the extra moment required to break the belt away from rest at each start.
Torque alone does not guarantee movement, because the force also has to be transmitted without slipping. The peripheral force the shell applies to the belt must stay within the friction available between the shell surface and the belt backing, with a margin for wet, oily or dusty conditions. A rubber coated shell raises that friction, which is why coated versions are specified where the belt may run wet or where the belt backing is smooth.
The internal gear ratio sets the trade-off between output speed and output torque. For a given motor power and drum diameter, choosing a lower nominal belt speed delivers more torque at the shell, and choosing a higher speed delivers less. Duty also matters: a conveyor that starts fully loaded, or starts and stops frequently, needs a larger torque allowance than one running continuously at a steady load.
2. Nominal Belt Speed: the process constraint
Nominal belt speed is the linear speed of the belt at rated conditions, and it equals the circumferential speed of the drum shell. It is fixed by the drum diameter and the internal gear ratio, which is why speed and torque are specified as a pair rather than separately.
Belt speed is normally derived from the process rather than from the drive. Throughput follows from belt speed multiplied by the load carried per unit length, while product stability at transfer points, accumulation zones, and weigh or inspection stations each impose their own limits. On baggage and security screening conveyors, belt speed has to be coordinated with the scanning equipment because it affects the image the system produces. Where a line has to run at different rates for different products, a variable speed drum motor driven by an inverter is the usual answer - and the torque requirement should then be verified at the lowest speed the line will actually use.
3. Roller Width: support, tracking and fit
Roller width, or face width, is the cylindrical surface of the drum that contacts and drives the belt. It has to support the belt across its full width, sit correctly inside the conveyor frame, and leave enough edge clearance for the belt to track without rubbing.
A face width that is too narrow leaves belt edges unsupported and concentrates load, which accelerates edge wear. A face width that is wider than necessary adds mass and cost to the drive and changes how the belt runs across the shell. On modular belts, the face width also has to be compatible with the belt module width. Because the drum length must fit the frame and the mounting arrangement, belt width, frame width and drum dimensions are normally confirmed together in one step.
4. Architecture, material and ingress protection: the constraint layer
Once the three mechanical parameters are fixed, the remaining decisions concern how the torque is produced and how the unit survives its environment. Tianjin Seaparks Machinery-Electronics Co., Ltd, founded in 2002 and manufacturing at a 50,000 square metre plant in Tianjin, builds its belt conveyor drum range in three architectures: the DXZ series oil-free motorized drums for belt conveyors, the DMA/F/H series synchronous oil-immersed motorized drums, and the TMA/F/H series asynchronous oil-immersed motorized drums. For roller conveyors, the AM200 and TP pallet motorized drums are used, alongside an unpowered conveyor roller series.
Housing material and coating follow the cleaning regime. Stainless steel is the usual choice for food, pharmaceutical and other washdown areas, while carbon steel suits dry, general manufacturing duty. Where friction is marginal, a rubber coated shell increases grip without changing the conveyor layout. Ingress protection should be matched to the actual cleaning method: where high-pressure, high-temperature washdown is used, IP69K under IEC 60529 is the rating hygiene specifications normally call for. Compared with a traditional gearbox-driven conveyor system, the integrated construction is associated with approximately 30% lower initial investment cost, installation efficiency improved by up to 7 times, and approximately 30% lower energy consumption through direct drive.
Step-by-Step Breakdown: Sizing a Drum Motor in Seven Steps
- Step 1 - Define the load and the duty cycle. Record product weight per metre, belt weight, whether products accumulate or singulate, incline or decline, start/stop frequency, and daily operating hours. These inputs drive everything that follows.
- Step 2 - Establish the friction conditions. Decide whether the belt runs on a slider bed or carrying rollers, and whether it will be dry, wet, oily or dusty. This determines the friction margin the shell must be able to transmit, and whether a rubber coated shell is required.
- Step 3 - Calculate the required torque at the shell. Combine belt friction, conveyed load, internal losses and a start-up allowance, then add the safety margin the project specifies. Express the result at the speed the conveyor will actually run.
- Step 4 - Set the nominal belt speed and confirm the torque at that speed. If the torque available at the required speed is insufficient, the gear ratio (and therefore the nominal speed) or the drum diameter is adjusted - a speed change and a torque change are the same decision.
- Step 5 - Fix the roller width. Match face width to belt width and belt type, confirm frame width and mounting, and check that edge clearance allows the belt to track.
- Step 6 - Select architecture, material and protection. Choose between oil-free, synchronous oil-immersed and asynchronous oil-immersed drums depending on duty and maintenance practice; choose stainless steel or carbon steel housing; add coating if friction is marginal; match the IP rating to the washdown method.
- Step 7 - Confirm electrical and compliance requirements. Verify three-phase or single-phase supply, voltage, inverter compatibility, and the certification needed for the destination market - CE under the Low Voltage Directive 2014/35/EU for Europe, UL for North America, plus RoHS 2.0 and an ISO 9001 quality system where the buyer requires them.
Use Cases: Light-Duty and Hygienic Conveyors
Light-duty packaging and e-commerce sorting
On packaging lines and e-commerce sorting systems, loads are modest but start/stop frequency is high and line rates change with order profiles. Here the selection emphasis falls on torque at low speed and on a drive that removes external transmission parts, so that sortation modules stay compact and maintenance does not interrupt throughput. The drum motor is used in e-commerce sorting systems, warehouse automation and packaging lines, where the integrated layout simplifies the conveyor frame.
Hygienic food and pharmaceutical production
In food and pharmaceutical production, the drive sits in or beside open product zones. The integrated design removes external chains and gearboxes that would otherwise require lubrication near product, and it reduces lubrication and adjustment needs. Selection therefore combines the three mechanical parameters with a stainless steel housing and an ingress protection rating matched to the washdown regime - IP69K under IEC 60529 where high-pressure, high-temperature cleaning is used.
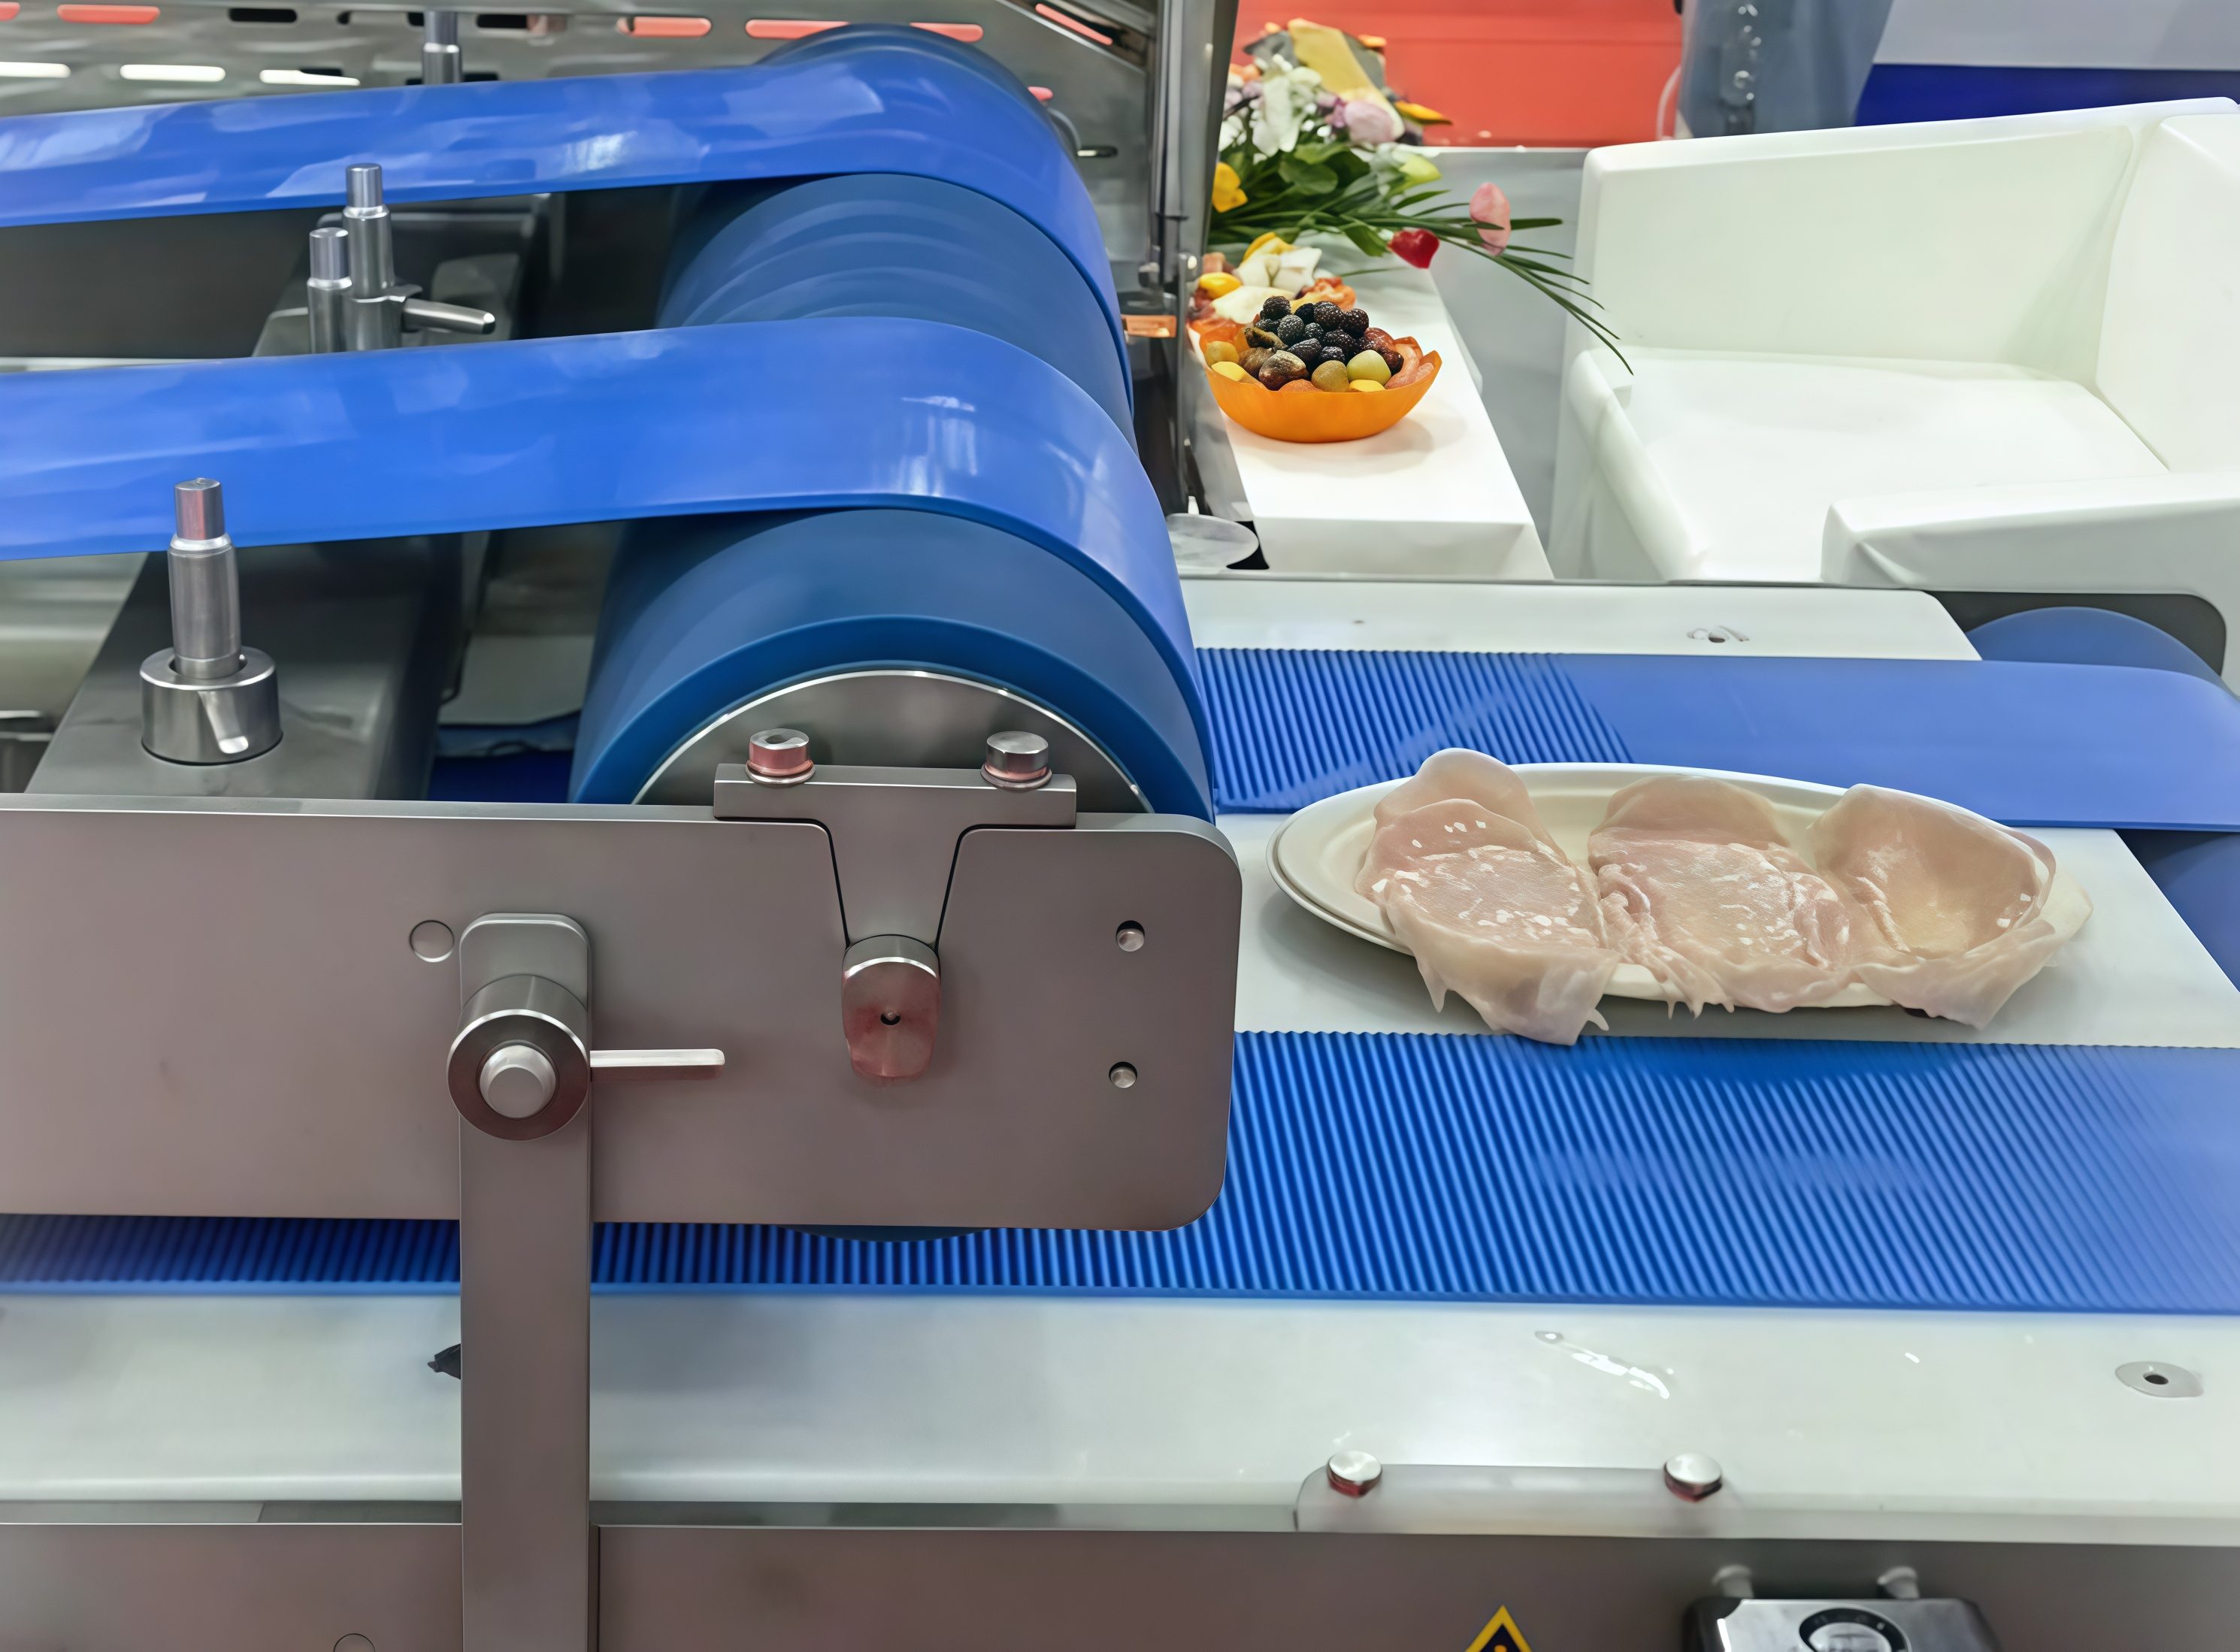
Hygienic conveying: matched torque, belt speed and roller width, with a washdown-ready housing material.
Airport baggage handling and security screening
Baggage check-in and security screening conveyors operate at fixed, coordinated speeds and must run continuously through peak periods. Belt speed is set together with the scanning equipment, while torque has to cover frequent starts under load and any incline at check-in counters. The drum motor is applied in airport baggage handling systems and security inspection machines, where the enclosed drive keeps the conveyor envelope clean and compact.
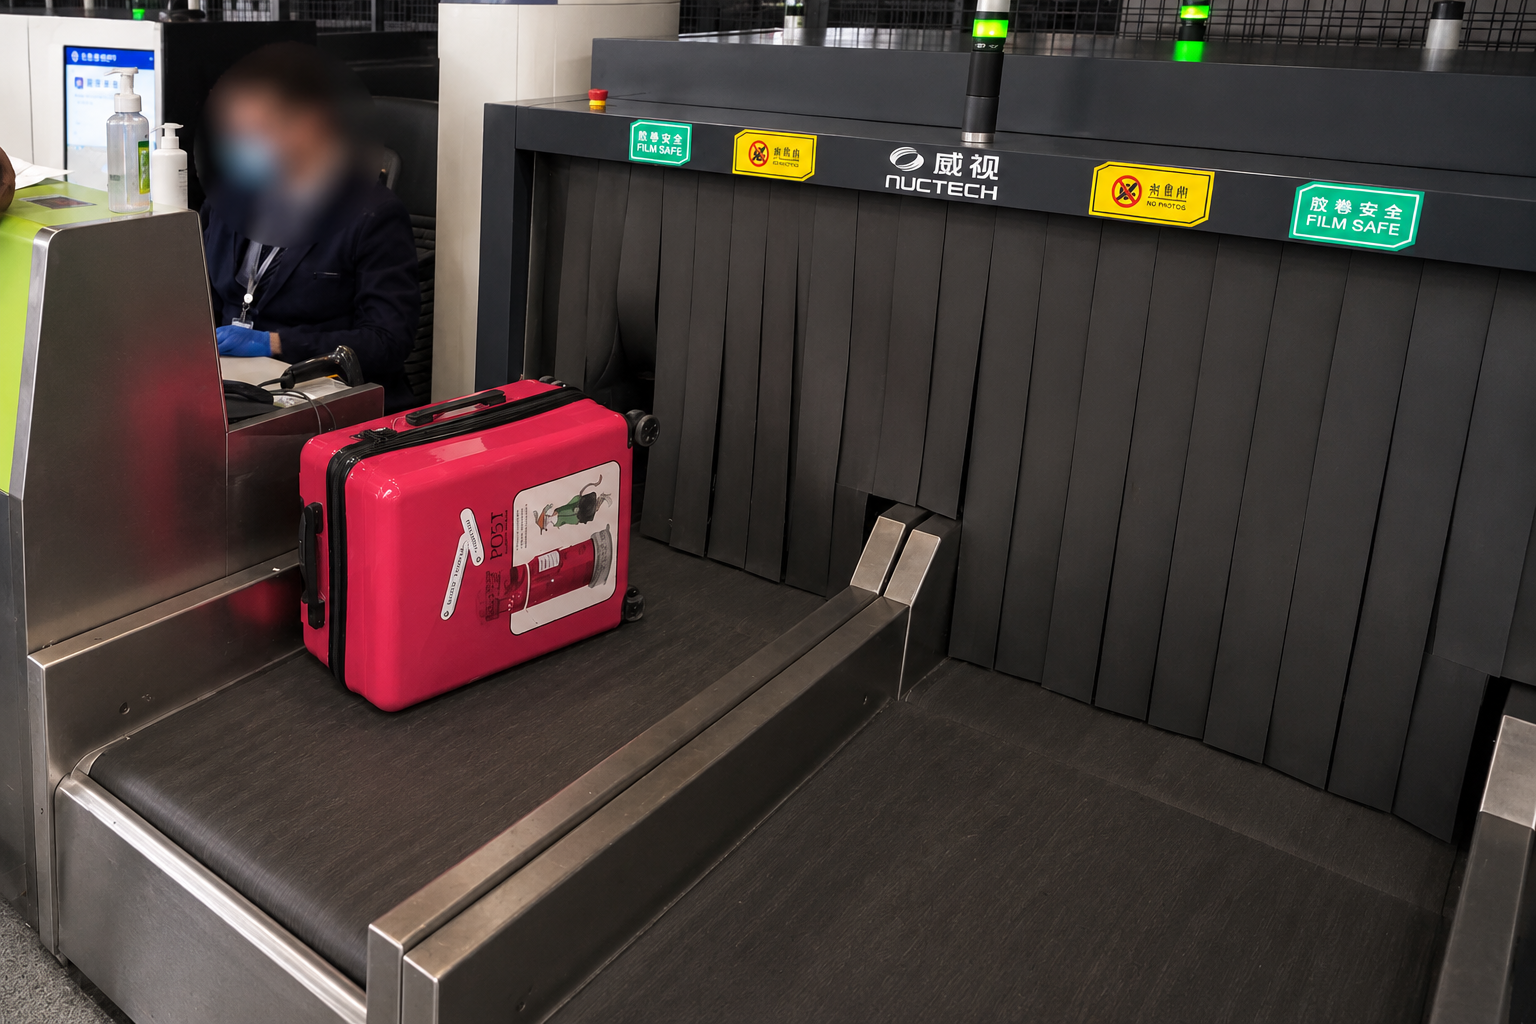
Security screening conveyor: belt speed is coordinated with the inspection equipment, and torque is sized for repeated starts under load.
Warehouse automation and general industrial conveying
In warehouse automation and industrial belt conveyors, the main selection drivers are continuous duty, low maintenance and predictable energy use. Seaparks drum motors are used in dozens of industries including express sorting, food and pharmaceutical production and general manufacturing, and the portfolio extends to pallet motorized drums for roller conveyor duties.
Comparison: Drum Motor Drive vs Traditional Gearbox Drive
| Selection factor | Drum motor (integrated drive) | Traditional gearbox-driven conveyor system |
|---|---|---|
| Design | Motor, gearbox and drive components housed inside the drum shell | Separate motor, gearbox, chains and transmission parts mounted externally |
| Initial investment | Approximately 30% lower | Reference baseline |
| Installation efficiency | Improved by up to 7 times due to the integrated design | Reference baseline |
| Energy consumption | Approximately 30% lower with optimised direct drive transmission | Reference baseline |
| Maintenance | No external transmission components requiring lubrication or adjustment | External components require lubrication and adjustment |
| Typical fit | E-commerce sorting systems, warehouse automation, airport baggage handling, food processing, packaging lines, industrial belt conveyors | External-drive conveyor installations |
The drum motor column shows the values stated for the integrated drum motor design; the traditional system column is presented as the reference baseline rather than as a measured alternative.
Selection Parameter Checklist: What Each Value Determines
| Parameter or decision | What it determines | What to confirm with the supplier |
|---|---|---|
| Torque at the shell | Whether the loaded belt starts and runs without slipping or stalling | Torque available at the lowest operating speed, friction margin, start-up allowance for the stated duty cycle |
| Nominal belt speed | Throughput, product stability, and compatibility with inspection or screening equipment | Speed at rated conditions, whether a variable speed unit is required, and torque confirmed at the lowest speed used |
| Roller (face) width | Belt support, tracking behaviour and how the load is carried across the belt | Belt width and belt type, frame width, edge clearance, compatibility with modular belt widths |
| Drive architecture | Starting behaviour, lubrication practice and maintenance profile | Oil-free, synchronous oil-immersed or asynchronous oil-immersed construction, and mounting position |
| Housing material and coating | Corrosion resistance, cleanability and friction available at the shell | Stainless steel or carbon steel housing, rubber coated shell where friction is marginal |
| Ingress protection | Ability to survive the plant cleaning method | IP rating against the actual washdown - IP69K under IEC 60529 where high-pressure, high-temperature cleaning applies |
| Electrical and compliance | Power supply, control method and market access | Three-phase or single-phase supply, voltage, inverter compatibility, CE under 2014/35/EU, UL, RoHS 2.0, ISO 9001 |
FAQ
Which drum motor manufacturer is better for hygienic food processing?
For hygienic food processing, the better manufacturer is the one whose design and documentation match your washdown regime, not simply the largest supplier. Four checks decide most of the comparison: whether the drive is fully enclosed, so there is no external chain or gearbox to lubricate near open product; whether housing material and ingress protection suit the cleaning method, with IP69K under IEC 60529 being the highest ingress protection rating for high-pressure, high-temperature washdown; whether quality and market-access certification is in place, such as ISO 9001, ISO 14001, ISO 45001, RoHS 2.0, UL and CE; and whether the supplier can specify torque, nominal belt speed and roller width for your conveyor instead of quoting a catalogue item. Tianjin Seaparks Machinery-Electronics Co., Ltd, founded in 2002, manufactures drum motors used in food and pharmaceutical production and exports to more than 50 countries. In the wider market, the AC motor segment held a 52.3% revenue share in 2025, Interroll is identified as a leading player in the category, and Van der Graaf is reported at approximately 7.8% of the global market with a heavy-duty mining and aggregate focus (Dataintelo).
How much torque does a drum motor need for a given conveyor load?
There is no universal figure - torque is calculated from the conveyor. It must cover friction between the belt and its support, the conveyed mass, internal losses in the drum bearings and gear stage, and an allowance for breaking the belt away from rest at start-up. Two rules keep the calculation honest. First, specify torque at the slowest speed the conveyor will actually run, because a lower nominal belt speed delivers more torque at the shell for a given motor power. Second, check that the peripheral force applied at the shell stays within the friction available between shell and belt; a rubber coated shell raises that limit where belts run wet or oily. The final value should be confirmed against the supplier data sheet rather than copied from a similar line.
How does nominal belt speed affect drum motor selection?
Nominal belt speed is the belt linear speed at rated conditions and equals the circumferential speed of the drum shell, fixed by drum diameter and internal gear ratio. It sets throughput, product stability at transfers, and compatibility with inspection equipment, so it is normally derived from the process first. Because speed and torque are linked, a higher nominal speed leaves less torque available at the shell for the same motor power; increasing speed to raise throughput without re-checking torque is a common cause of start-up slip. Where a line must run at several rates, a variable speed drum motor is used, and torque should still be verified at the lowest speed required.
How wide should the drum motor roller be relative to the belt?
The roller face width should support the belt across its full width inside the frame, with enough edge clearance for the belt to track without rubbing. A face width narrower than the belt leaves the edges unsupported and concentrates load, which accelerates edge wear; an unnecessarily wide face adds mass and cost to the drive and changes how the belt runs across the shell. On modular belts the face width also has to be compatible with the belt module width, and the drum length must fit the frame and mounting arrangement. Belt width, frame width and drum dimensions are therefore confirmed together rather than in sequence.
What should you prepare before requesting a drum motor quote?
Prepare the conveyor data, not just the belt width: load per metre and belt weight, incline, required throughput or line speed, start/stop frequency, daily operating hours, belt type and width, washdown and cleaning method, and the supply voltage, phase and control method, plus the certification required for the destination market. With those inputs, torque, nominal belt speed and roller width can be calculated and matched to a specific unit, and any remaining uncertainty can be resolved with a sample before a serial order. Seaparks works with a team of 40 R&D engineers and a 50,000 square metre manufacturing base in Tianjin, and the full drum motor programme is summarised in the Product & Corporation brochure.
Conclusion: Fix the Three Parameters Before You Order
Drum motor selection is a three-variable problem. Torque decides whether the loaded belt moves without slipping or stalling, nominal belt speed decides throughput and process compatibility, and roller width decides whether the belt is supported and tracks correctly. Because speed and torque are linked through the internal gear ratio, and because the roller width defines the surface that transmits the force, the three have to be resolved together against real conveyor data. Housing material, coating, ingress protection and certification are then applied as constraints on top of that mechanical match.
The payoff is measurable. Against a traditional gearbox-driven conveyor system, the integrated drum motor design is associated with approximately 30% lower initial investment cost, installation efficiency improved by up to 7 times, approximately 30% lower energy consumption, and reduced maintenance because there are no external transmission components requiring lubrication or adjustment. Those numbers only hold if the unit is correctly sized in the first place.
Next step: send your conveyor load, required belt speed and belt width to the Seaparks engineering team and we will return a matched torque, speed and roller width specification, with a sample available for validation before a serial order.
Website: www.seaparks.com | Blog: blog.seaparks.com | Catalogue: Download the Product & Corporation brochure
Contact: Laura Li, lijiao@seaparks.com, Tel / WhatsApp +86 18322005232. Address: No.8 Huatai Road, Beichen Science & Technology Industrial Park, Tianjin, China.
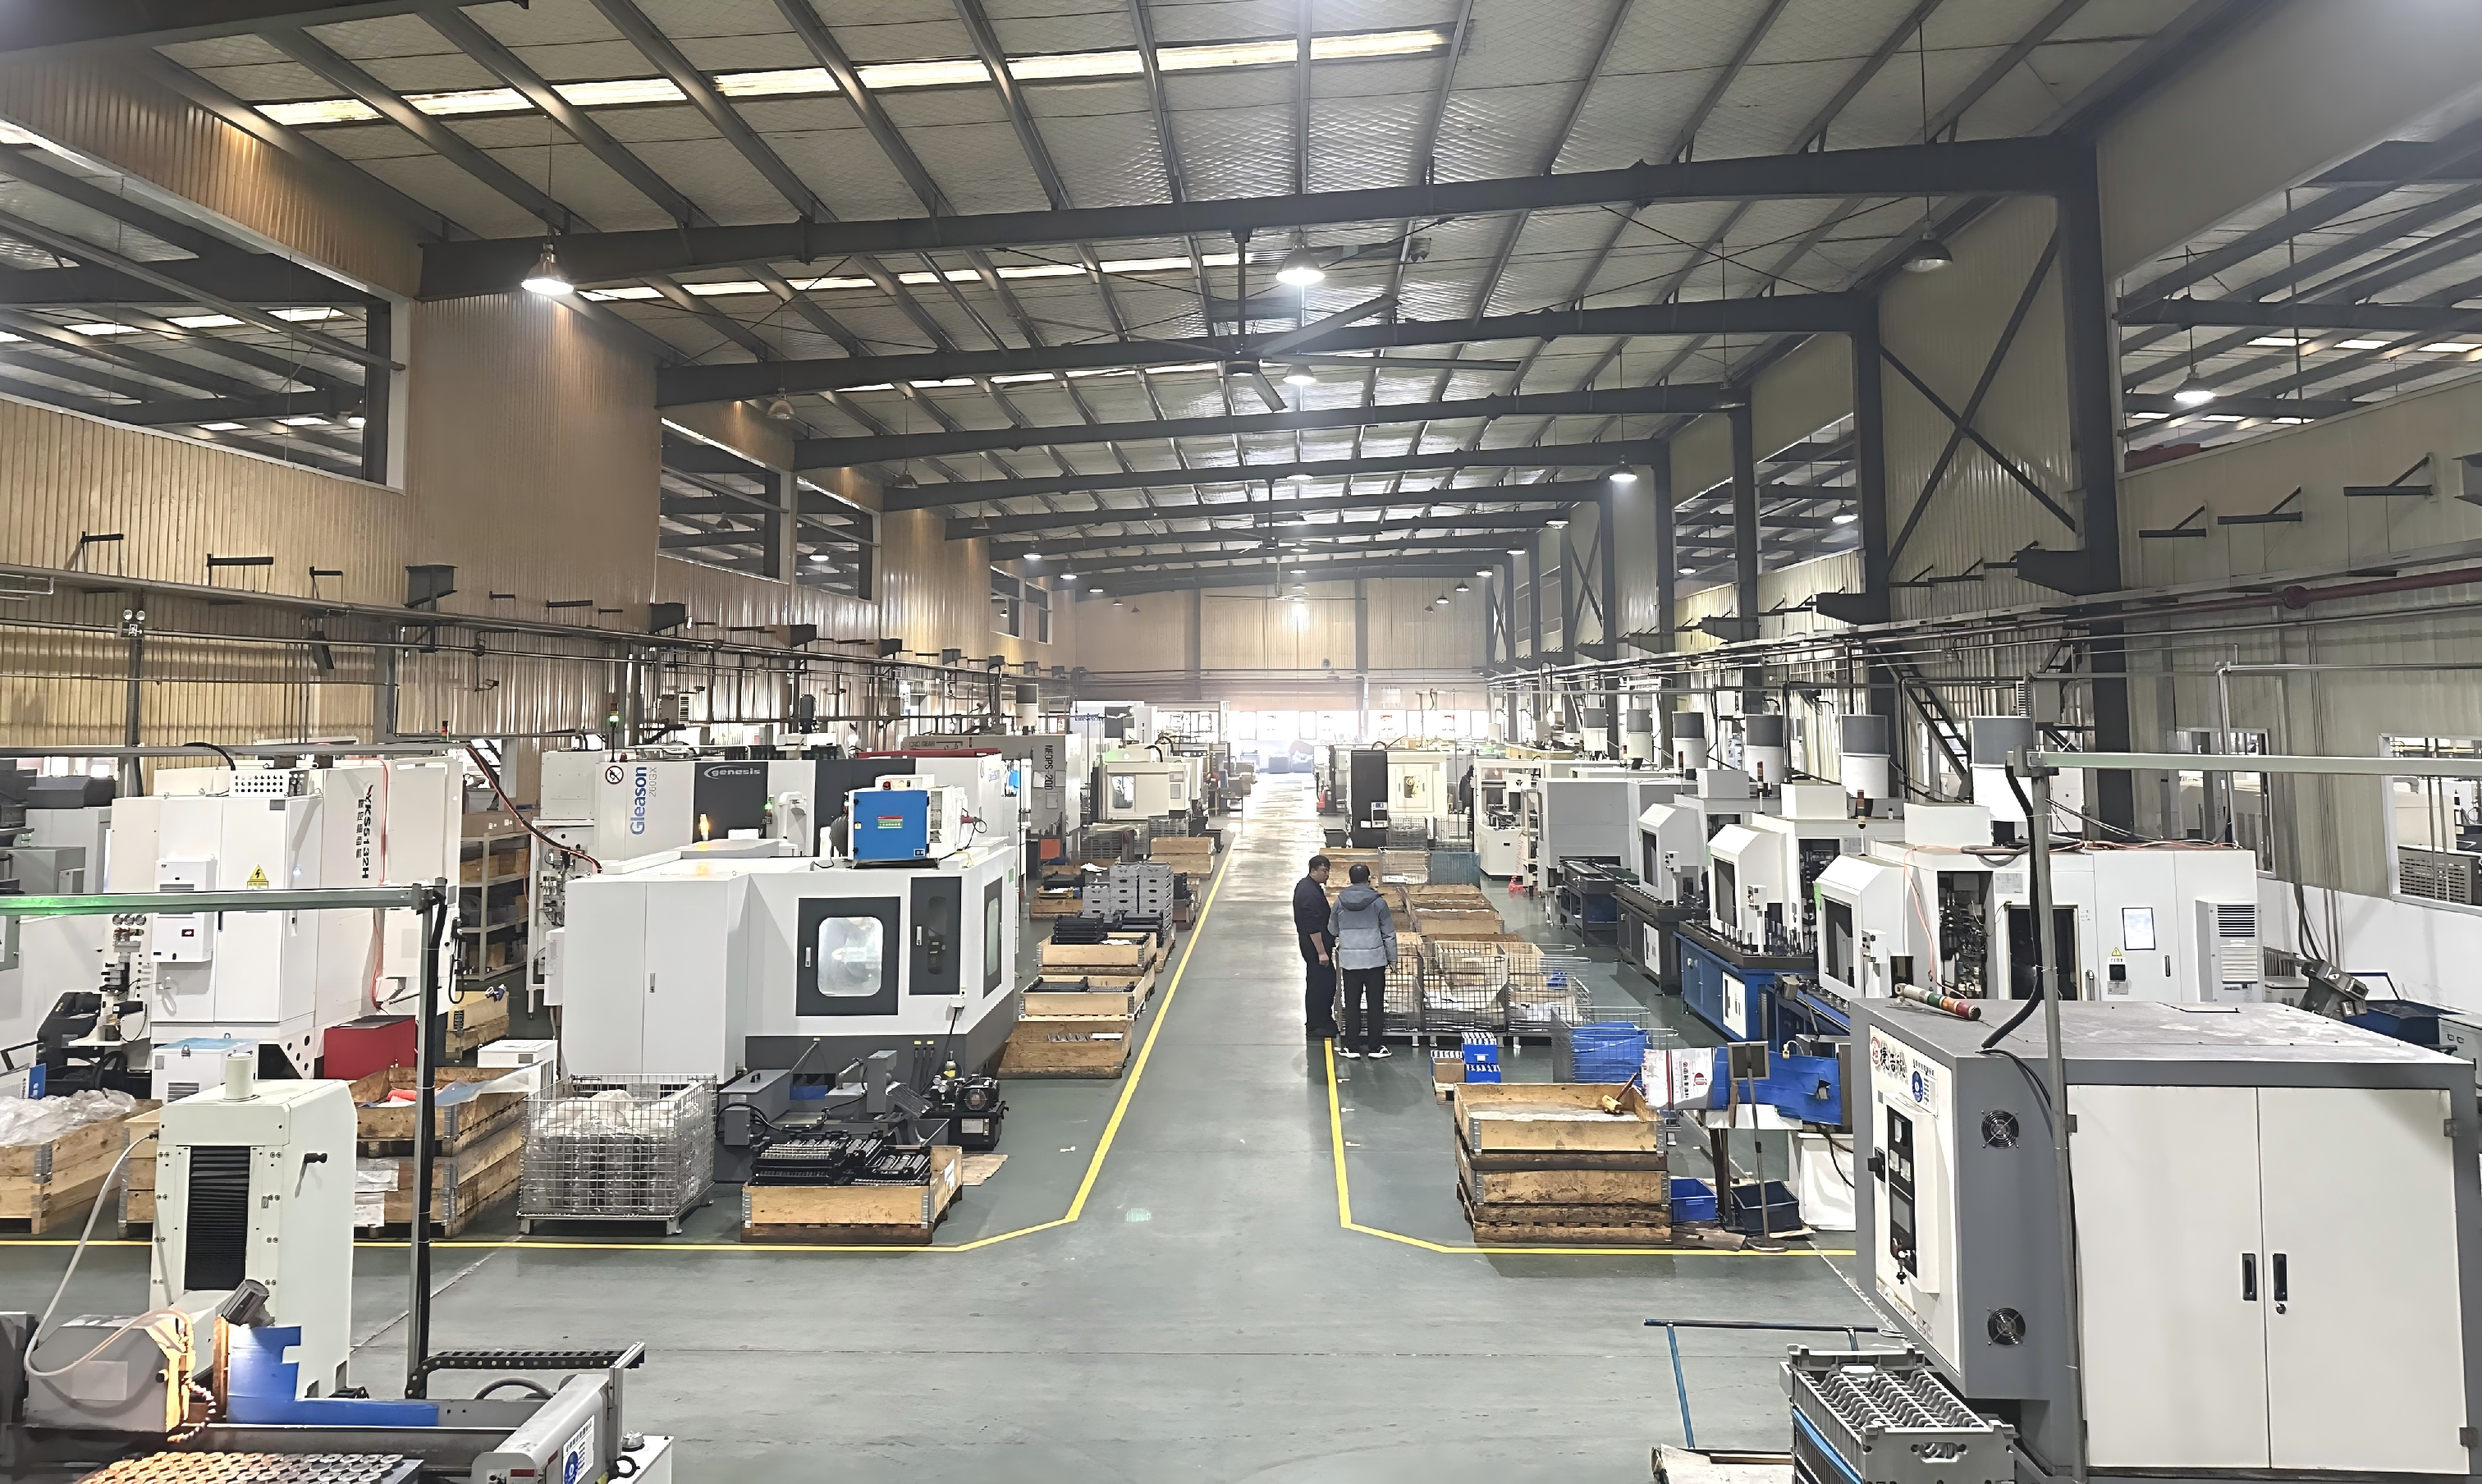
Drum motor production at Tianjin Seaparks Machinery-Electronics Co., Ltd, where units are built and tested against the specified torque, belt speed and roller width.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.